PROBITERS INDUSTRIAL COMMAND CELL REF CODE: PRO-SPM-2026
✓ NABL / CE CERTIFIED ARCHITECTURE
4 Spindle Torquing System
Control Engine Siemens / Mitsubishi
Delivery Guarantee Production-Ready

4 Spindle Torquing System

Four-station simultaneous torquing cell for two-wheeler assembly.

Control systemMitsubishi FX5u
HMIMitsubishi GT2000
Process4-station simultaneous torquing
OutputLogged torque + angle per station
After-sales support3 months free, until production-ready
Typical quote turnaround3–5 working days
Target Plant Applications:
Automotive / two-wheeler assembly
FIELD-PROVEN CASE STUDY • GIDC Sanand, Gujarat

Tier-1 Automotive Engine & Transmission Assembly Line

PROBITERS ROI: 4.9 Months PAYBACK
❌ Competitor Machine Pitfalls

Manual pneumatic torque wrenches suffered operator fatigue, uncalibrated torque drift (±12%), and zero audit trail, leading to customer quality defect claims.

❌ Impact: High Scrap Rates & Unplanned Supplier Delays
Probiters Engineering Advantage

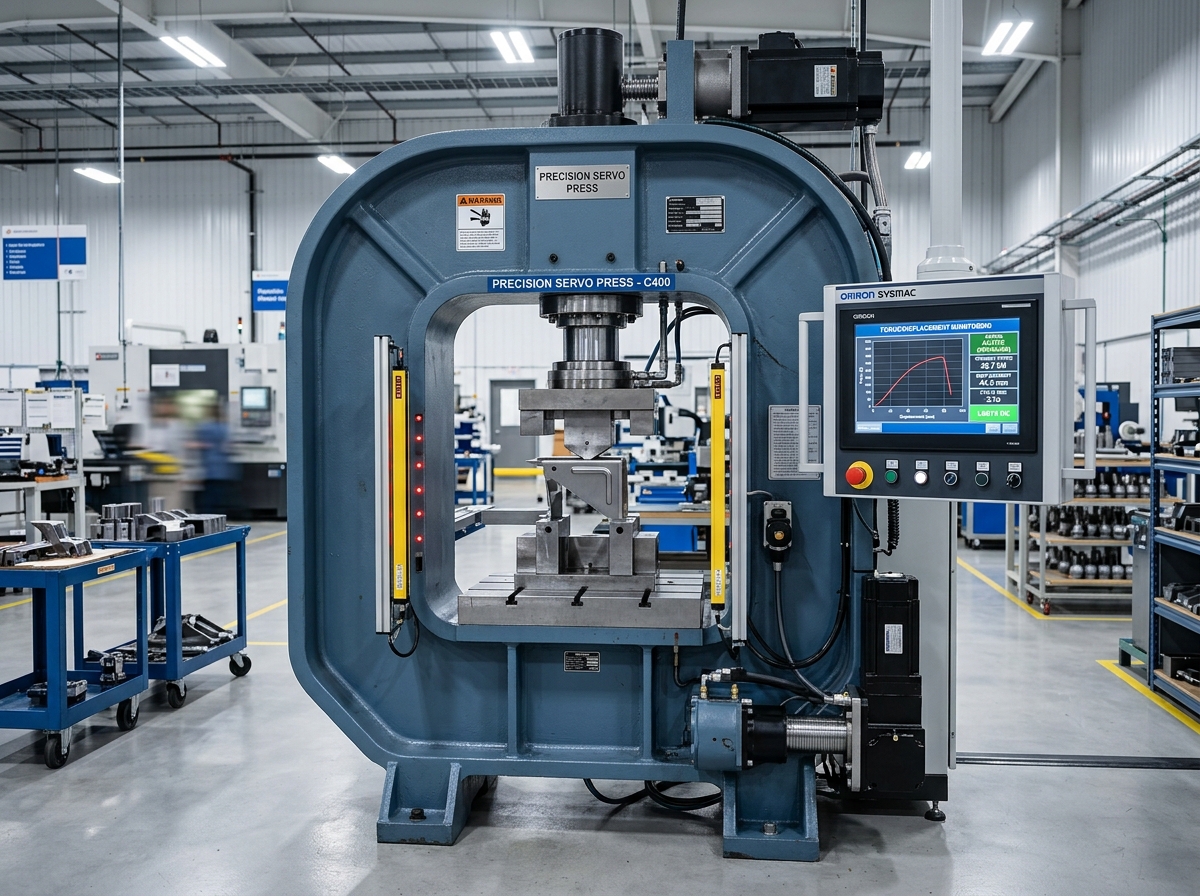
Probiters 4-Spindle Synchronized Servo Torquing Rig featuring multi-stage angle/torque monitoring, automatic fastener feeder bowl, Poka-Yoke sensors, and MES database sync.

Support Commitment:
100% Traceability MES Software Sync & On-Site Torque Calibration
✓ Verified Financial Outcomes & ROI
Payback Period 4.9 Months
Annual Savings ₹19.6 Lakhs / yr
TORQUE ACCURACY DRIFT ±12% Drift Reduced to ±1.5% Zero Field Warranty Recalls
"Every bolt tightened on our engine casing is recorded in our MES with exact torque-angle graphs. Probiters eliminated warranty recall risks completely."
Get Custom ROI Proposal →
Engineering Enrichment

Machine Engineering Dossier

Specifications, datasheet, GA concept and product catalogue — built in the same Probiters design language.

Request Machine Proposal

Configuration & Pricing

Final pricing depends on configuration, size and tooling package. Most systems in this category are quoted within 3–5 working days — priced to compete with imported and OEM alternatives.

Request a Quote
On-time delivery commitment
Free support to production-ready
Design intent

Four-station simultaneous torque-controlled assembly system with logged torque and angle per station.

A multi-spindle assembly station designed to tighten four fasteners in a controlled sequence or simultaneously. The system combines guided fixtures, torque-controlled spindle drives and recipe-based tightening parameters to reduce assembly variation.

Engineering problem: Manual tightening can produce variation in torque, angle and sequence. A multi-spindle system controls the tightening strategy and records the result at each station.

Applications

Typical use

Automotive component assemblyPowertrain subassembliesFlange and multi-bolt assembliesIndustrial fastening
Open product catalogue
Process architecture
01LOADLoad component into fixture
02VERIFYVerify part presence and fastener readiness
03POSITIONPosition four spindle heads
04RUNRun programmed torque/angle sequence
Engineering data
ParameterDesign basis / published information
Control systemMitsubishi FX5u
HMIMitsubishi GT2000
Process4-station simultaneous torquing
OutputLogged torque + angle per station
Typical torque envelope5–200 Nm per spindle, tooling dependent
Spindles4 independently monitored
Fastener rangeApplication-specific
Result logicTorque/angle windows + sequence validation
COMPLETE ENGINEERING PACKAGE

Need Full Technical Specifications & GA Drawings?

Need the complete engineering package? Open the specification, datasheet and GA drawing. Final tooling, dimensions, cycle time and acceptance criteria are engineered around the customer's part and process.

View full specification